Test rest
Test rest
Test rest
Two-part silicones are used for potting electronic assemblies, encapsulating electronic components, and making molds for cast urethane rubber. Each part contains functional ingredients, and the two parts are mixed together in a specific ratio. The entire system requires curing so that the silicone hardens and acquires its end-use properties. Curing, the crosslinking of polymer chains, is a chemical reaction that is accelerated using a catalyst. Sometimes, post-curing is also used. For design engineers who want to learn more about curing systems, this Gluespec Q&A answers frequently asked questions (FAQs).
Two-part silicones that are used for potting, encapsulating, and mold making are usually either addition cured, or condensation cured. Addition curing uses a platinum catalyst for crosslinking or curing. Condensation curing uses an organotin catalyst instead. These are not the only curing systems for silicones, but they are the most common types for the two-part silicones that are used in potting, encapsulating, and mold making.
Addition cure silicones have quick curing times and very low shrinkage rates. Importantly, they are not subject to reversion, an unwanted process that returns a catalyzed silicone to a liquid state. Addition curing is also less prone to silicone migration, which can contaminate electronics, and provides more durable coatings. Plus, post-curing is not required for the silicone to achieve its ultimate properties. This reduces curing costs and speeds cycle times.
Cure inhibition, or catalyst poisoning, can occur if an addition cure silicone contacts amines, sulfur, phosphides, PVC plasticizers, sulfur vulcanized rubber, some epoxy resin catalysts, or tin catalyzed silicones. Cure inhibition is also caused by contact with the latex, vinyl, or neoprene gloves that workers wear to handle assemblies. In machine shops, oils in the air can cause mild cure inhibition. There is also the potential for cure inhibition if there is contact between an addition cure silicone and acrylics.
Accelerated curing with heat, the careful control of substrates, and using an additional catalyst have all been shown to be effective in overcoming cure inhibition.
Condensation cure silicones work well with most substrates and resist cure inhibition. They are not subject to reversion if the cured silicone has access to the atmosphere. They have a relatively low risk of cure failure and can support deep section curves.
Condensation cure silicones are not the best choice for use with SBR rubber. They also have the potential for reversion if the silicone is totally enclosed and subject to heat and/or pressure over time. For example, reversion may occur if a condensation cured silicone is subjected to 150°F temperatures in a completely sealed environment for a period of several months.
No, they do not. The moisture that is needed for crosslinking is included in the system.
One-part silicones are also available for potting, encapsulating, and mold making. For example, one-part room temperature vulcanizing (RTV) silicones are typically moisture cured. The moisture that they need for curing usually comes from the atmosphere. There are also one-part heat cured silicones that use an addition curing system. Because heat initiates cross-linking, the system components can be combined in an easily handled package and crosslinking will not occur until heat is applied.
What is vacuum bagging?
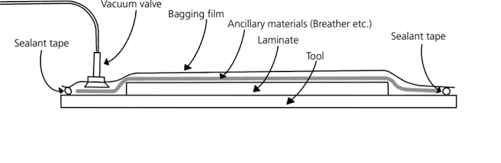
Vacuum bagging (or vacuum bag laminating) is a clamping method that uses atmospheric pressure to hold the adhesive or resin-coated components of a lamination in place until the adhesive cures. (When discussing composites, “resin” generally refers to the resin system— mixed or cured resin and hardener—rather than unmixed epoxy resin.)
Modern room-temperature-cure adhesives have helped to make vacuum bag laminating techniques available to the average builder by eliminating the need for much of the sophisticated and expensive equipment required for laminating in the past. The effectiveness of vacuum bagging permits the laminating of a wide range of materials from traditional wood veneers to synthetic fibers and core materials.
SILICONE FOR VACUUM BAG
Silicones for Producing Reusable Vacuum Bags
General Attribute
Applications
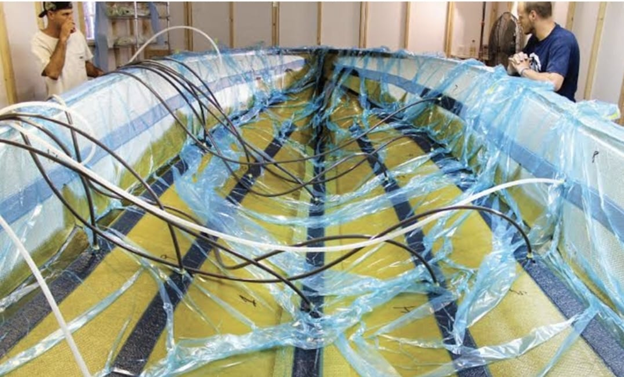
How it works?
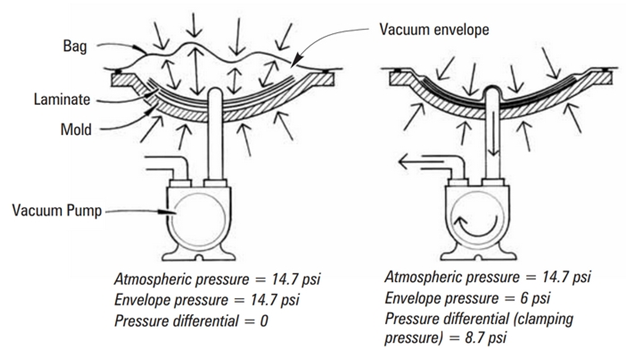
Vacuum bagging equipment
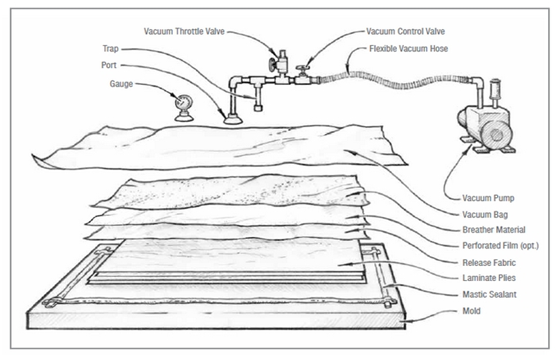
The vacuum bagging system consists of the airtight clamping envelope and a method for removing air from the envelope until the epoxy adhesive cures. This section discusses the components of this system , which include both specialized equipment and commonly available materials.
Vacuum Bagging Materials
Our product benefits
MAJOR APPLICATIONS
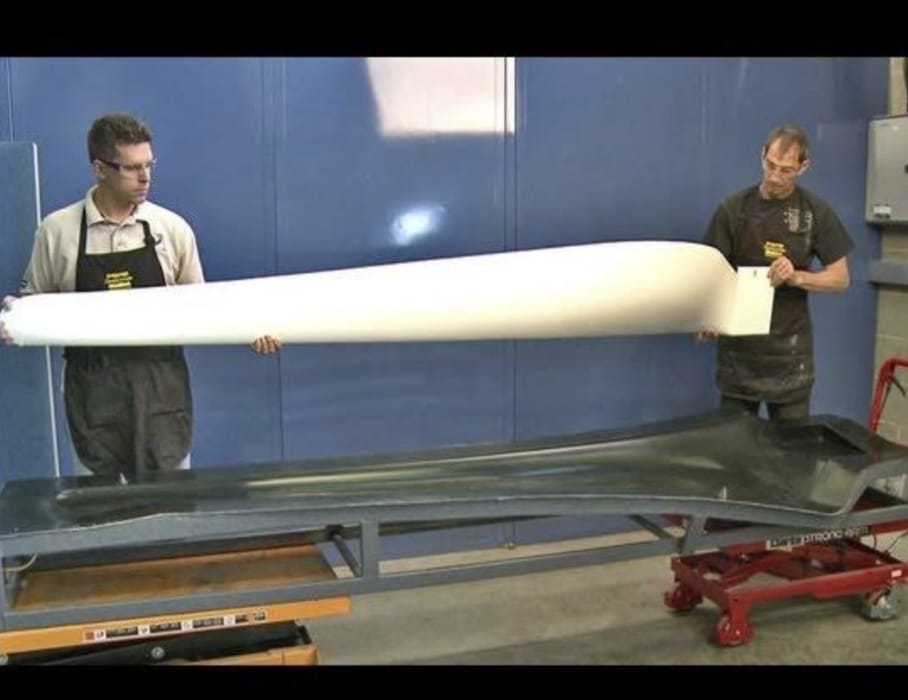
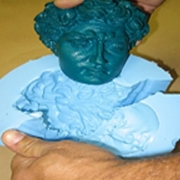
Silicone elastomers are designed with either addition (platinum) cure or condensation (tin) cure chemistry. Addition curing systems are 2-part liquid silicones that utilise a platinum catalyst to cure by either room temperature vulcanisation (RTV) or heat to accelerate cure.
Addition cure silicones do not produce by-products during the crosslinking (curing) process. The cure chemistry takes place internally, making them ideal for moulds or parts that are manufactured in a sealed environment. Addition cure silicones have very low shrinkage properties with great dimensional stability when exposed to either humidity or heat. This type of chemistry should be considered if the final mould will be stored for long periods of time between use.
Addition cure silicones can be used with various resins and materials including concrete, stone, brick, fibre glass filled resin, polyurethane, polyester, acrylic resin, and even another addition cure silicone.
General mouldmaking, Prototyping, Dental replication, Food moulding, Architectural replication & sculpting, Composites/fibre glass part production, Tampo pad printing, Special effects, Prosthetics & orthotics
When working with addition cure silicones, it is important to avoid inhibiting the cure process by bringing the uncured material into contact with certain chemical compounds. The poisoning of the cure catalyst stops the crosslinking necessary for the silicone to properly cure. The result of inhibition is tackiness at the pattern interface or a total failure of the silicone to cure.
Materials known to inhibit cure are sulphur-containing modeling clays, natural rubber such as latex and rubber gloves, masking tape, amine or sulphur-containing material, condensation cure (tin-catalysed) silicones, PVC stabilizers, and epoxy resin catalysts.
Manufacturers in aerospace and aviation have used silicones since their inception, however not everyone is familiar with all of their capabilities. Silicones seal joints, coat and encapsulate electronics and insulate and shield sensitive equipment from extreme temperatures and weather exposure. The versatility of silicone and its high temperature resistance have made it a reliable choice for decades and today it is still one of the most effective materials used in aerospace and manufacturing.
Silicone supports engines that experience high temperatures during liftoff, as well as on the exterior of a space capsule that experiences low and high temperatures and needs shock absorption when re-entering Earths atmosphere. Silicones effectiveness and versatility make them suitable for atleast 20 different areas of a launch vehicle.
RTV Silicone Rubber:
RTV Silicone rubber is short form of room temperature vulcanization silicone rubber. Once part A and part B mixed together at normal room temperature, it will create High flexible to medium flexible rubbers. RTV silicone is available in a variety of viscosities-ranging from low viscosity options that can be incorporated with additives to boost the thermal protection properties, to high viscosity formulations that can be applied to overhead surfaces.
Aviation applications
Aircraft applications
Other benefits of room temperature vulcanized(RTV) silicones
Electronics applications

Flexible Epoxy and Silicone Rubber
Polishing resin is a relatively simple process that just takes a little patience and effort. This instructable will address how to polish resin to a high gloss. The same methods I will address in this how to, apply to all cast resin polishing, and can be used to polish virtually any type of resin be it polyester or epoxy based.
The method first starts with some good old fashioned detail sanding working up through the grits, from very rough, to a very fine wet sanding. Then we move into two different grits of polishing compounds, and finally finish everything off at the buffing wheel using two very fine polishing abrasives, and finally, a carnuba wax polish to buff everything to a bright shine.
When done correctly, well polished resin casts and parts look absolutely amazing, and are works of art, ready for display, jewelry and enjoyment in and of themselves.
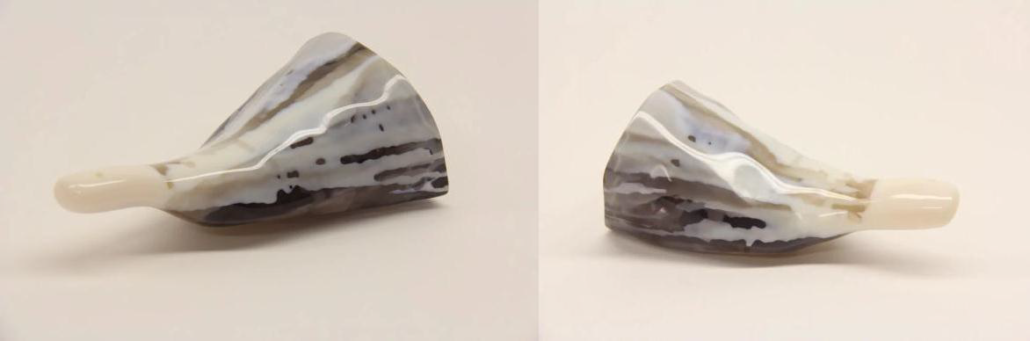
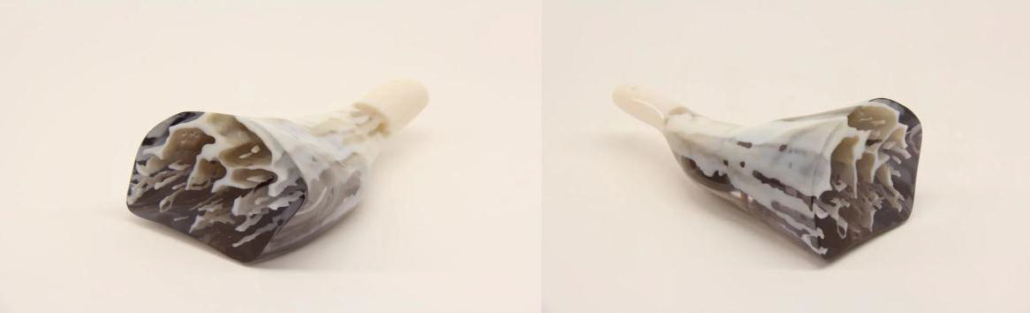
Step 1: Cast Part
The support material is a waste product of the print and must first be cleaned off before polishing can begin. Use a pressure washer, surform tools, dental tools.
If you are polishing a cast resin part, clean the outside of the resin with soap and water to remove any mold release that may be on the part.
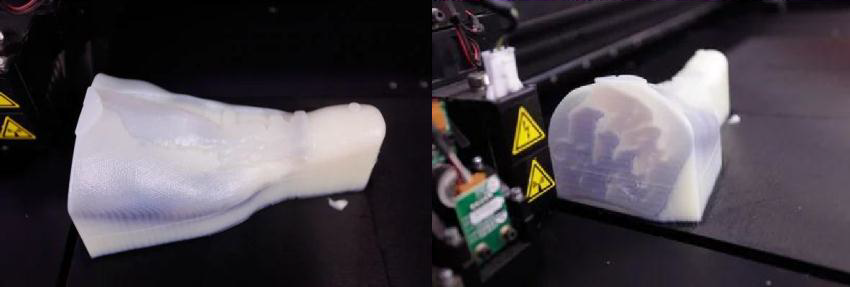
Step 2: Tools and Materials
Gather the tools and materials below to polish your resin part: sand paper 120, 180, 220, 400, 600, 800, 1000, 1500, 2000 grit. sanding block water.
scratch remover compound polishing compound
Lint free, scratch free polishing cloth mothers polishing ball Buffing wheel buffing compounds wax product
While there are many different buffing compounds and waxes available, I went to a regular car parts supplier box store and purchased low cost but totally effective rubbing compound made by Turtle Wax for car scratches, a Mothers Polishing Ball with a drill attachment and some Mothers Carnuba Car Wax
Step 3: Sand Paper Grits – From 120 to 2000
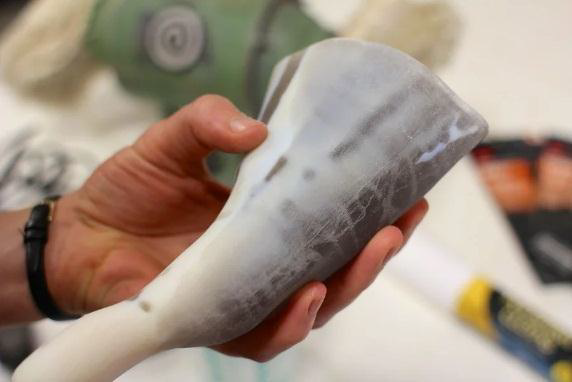
Start sanding the resin with 120 grit sandpaper. Make sure to sand all the surfaces of the resin part before going up to the next grit paper. It’s much easier to notice a deep scratch once the resin is sanded smooth and begins to become polished. The bummer with that however is that you’ve then got to backtrack all the way back to the beging and spot sand the blemish out. A better method is to sand the entire part comprehensively with the rough paper before moving up a grade.
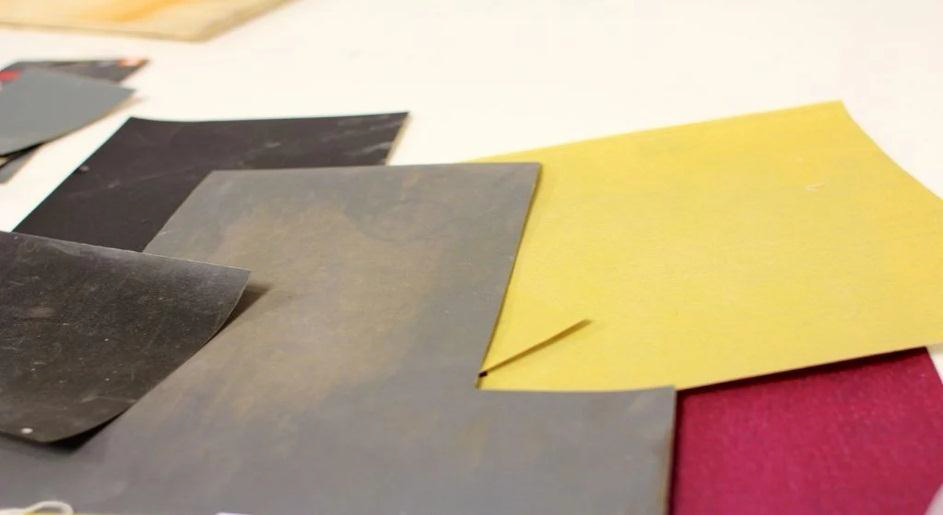
Step 4: Hand Sanding
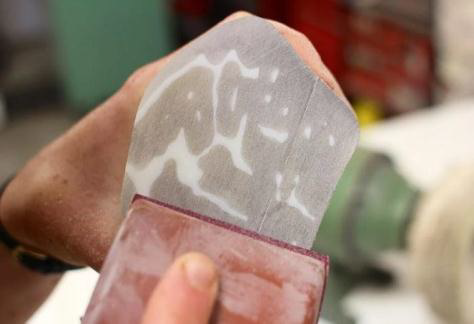
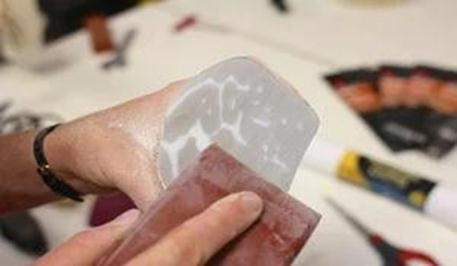
When we began polishing this piece of resin we were exclusively hand sanding. we took turns and rested before moving up to the next grit paper.
We used the sanding block only for the one flat side on this model, the rest of the time we just used our hands as a backer.
We experimented a bit using flexible foam sanding pads, and sponge-like backers on the sandpaper, but all in all, our hands proved to be a pretty effective and flexible support for the paper to get inside all the detailed contour sand crevices.
Step 5: Power Sanding
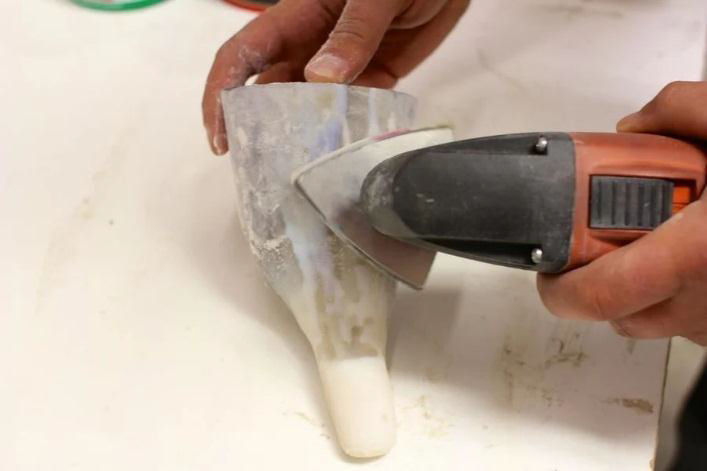
Larger sanders that one would want to use if you were working with a larger piece of resin.
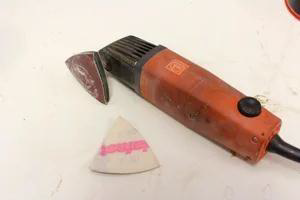
It’s easy to make custom sanding pads of the finer grit sanding papers for the detail sander. Simply take a spent Fein brand pad, spray it down with 3M adhesive, and slap a piece of fine sandpaper on it that’s been cut down to the same size. Presto – cheap and reusable fine grit sanding pad.
Step 6: Wet Sand by Hand
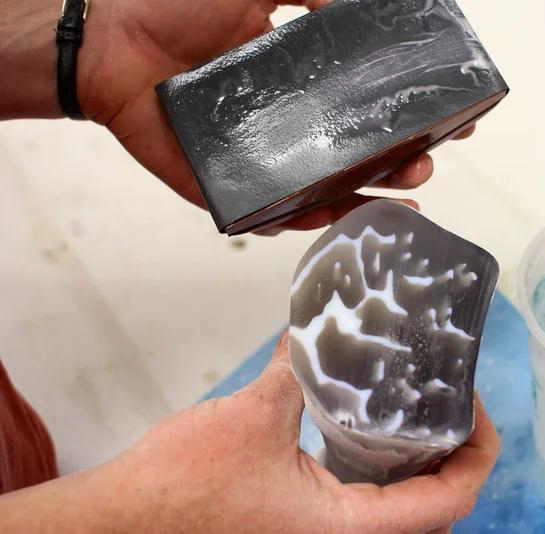
Once you get to 400 grit or so, depending on the type of sandpaper that you are using, it’s time to start wet sanding.
This process we did by hand for more control, and so we wouldn’t get electrocuted. Start sanding at 400 and work your way up to 600, 800, 1000, 1500 and finally, 2000.
Step 7: Check for Scratches
We found it easiest to check for scratches by completely wiping down the resin with a clean towel and then wetting it down with water. If you rub the water in a bit with your fingers it helps to bring any potential scratches, pot marks and inconsistencies out for inspection.
If the resin passes the scratch test, keep on sanding all the way up to 2000. By 2000 it should start to look pretty clear, but not polished. That comes in the next step.
Step 8: Rubbing Compound
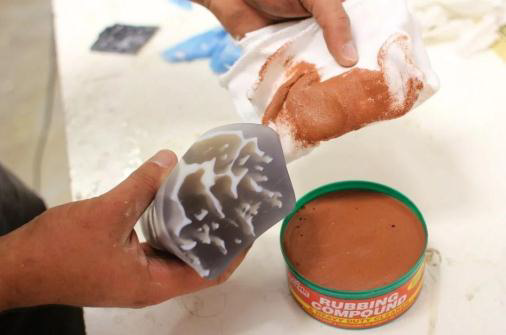
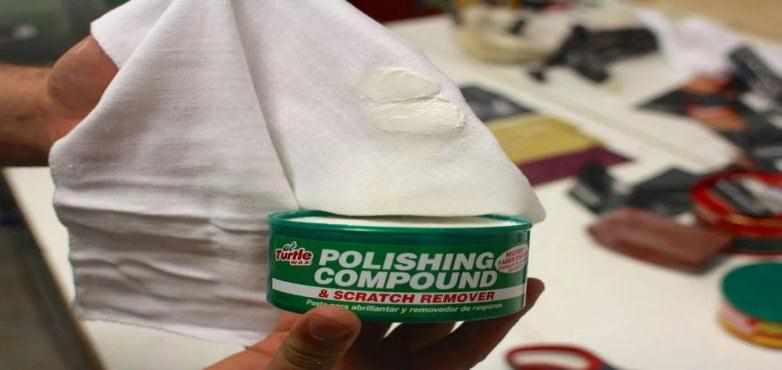
I used two different polishing compounds to start the polishing process – first was Turtle Wax brand Rubbing Compound.
Follow the instructions – apply a small amount to a clean polishing cloth and rub it vigorously onto the surface of the resin. Let it sit for a second and then buff it off with another part of the cloth.
This polishing compound is a finer grit than the sandpaper, but not quite as fine as the buffing compounds that are used on the mechanical buffing wheel.
Step 9: Polishing Compound
Follow the same procedure as described in the previous step for the finer of the two polishing compounds – Turtle Wax brand Polishing Compound.
This creamy white polishing compound really starts to bring out the initial polished surface in the resin…and in the next steps it just gets better and better.
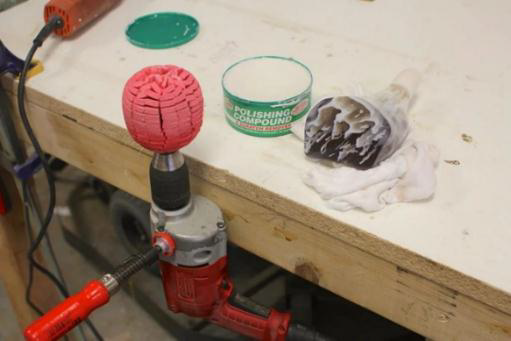
Step 10: Mechanical Polishing With Mothers Ball
While we preformed the previous two steps by hand with a polishing cloth, I thought it’d be useful to try a mechanical solution to this process as well. I picked up a Mothers Ball polishing tool at the car parts store and loaded into the chuck of my corded drill.
Lock the drill trigger on, load the ball with polishing compound and polish all the surfaces of the resin piece. Hold on to the resin piece as the drill spins. It doesn’t have much friction, but if it caught en edge on the resin piece, it’s possible it might try to come away from your hands.
Where an apron as this step tends to flick polishing compound around and about.Since this photo was taken I’ve begun polishing these models on the drill press, as it spins the ball with a bit more stability and speed control
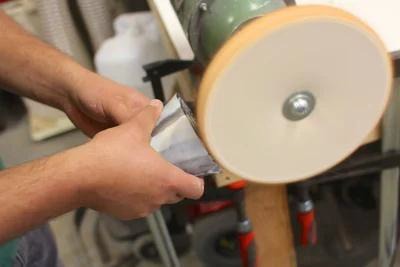
Step 11: Buffing Wheel – Tripoli
After polishing comes buffing on the motorized buffing wheel. Any motor that rotates at around 1500 – 2000 rpm will suffice. Mount the first all-linen buffing wheel in the kit to the arbor and load the wheel with tripoli compound. Again, I’m using a buffing kit from Beall Tool, but any buffing compound system that you’d like to work with will work just as well.Loading the wheel with compound means holding the bar to the wheel for a few seconds. Once some red material is deposited on the wheel, it’s good to go. If you are buffing a large area, you may need to reapply compound to the wheel.
Hold the resin piece tightly in your hands and engage it into the wheel.Always have the wheel spin down and away from you, and always buff on the bottom of the wheel in case something catches an edge – otherwise it will get launched right at you. If you buff down and away, it will at least get launched away from the operator.Always hold on to the part you are buffing with two hands, and try not engage any hard edge against the wheel. Better to buff the surface of the resin part parallel to the face of the buffing wheel, and never perpendicular to it as it has a tendency to “grab” the part.Keep the resin moving across the buffing wheel, never staying in the same place too long. The process builds up significant heat and we want to keep things cool by keeping everything on the move.
Step 12: Buffing Wheel – White Diamond
The Beall Kit’s next step is a diamond buffing compound. It gets used on a softer wheel than the first, so swap wheels, load up the new linen/cotton blend wheel with white diamond compound, and use the same buffing technique described
in the previous step.
It’s possible to buff the entire model – even concave areas by using different parts of the wheel, and even digging into the corner of the wheel if needed for smaller, detail areas
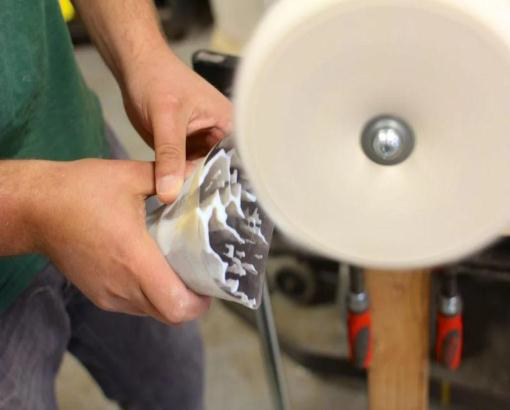
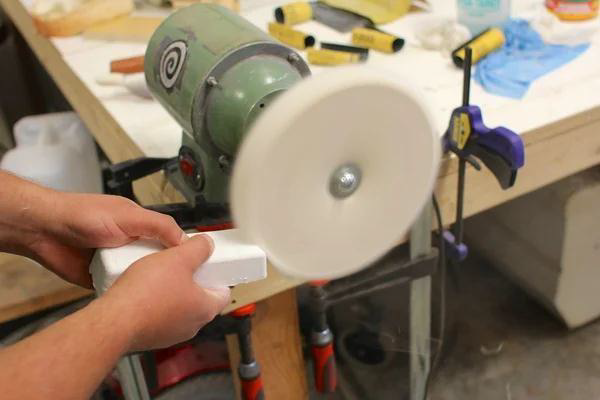
Step 13: Finish With Carnuba Wax
Swap wheels one last time to the all flannel wheel and load it with just a little bit of carnuba wax.
The more wax you load on the worse the final buffing will be since too much wax will build up upon the surface and ruin your finish! Just touch the carnuba wax bar to the wheel and load it up for a second or two. You can always reapply more later.
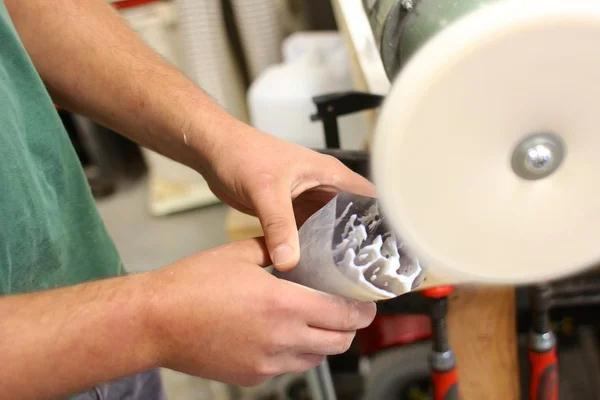
Step 14: How to Polish Small, Highly Detailed Parts Hands Free (hopefully)
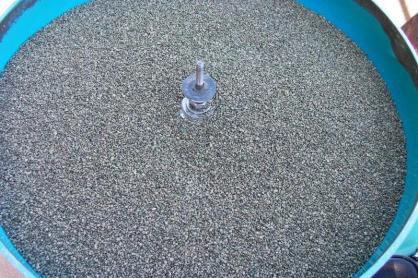
I am currently working on a completely automated, “hands off” version of this process using lapidary equipment – a vibratory polisher and different abrasive mediums.
I hope to be able to achieve the same results over several hours or days of parts vibrating in different grit medias that could run unattended, except for the changing of the media as the part moves up the grits.
I’m also going to test spraying a clear high gloss resin, as well as flame polishing any surface too detailed, or too small to sand in order to achieve a glossy finish.
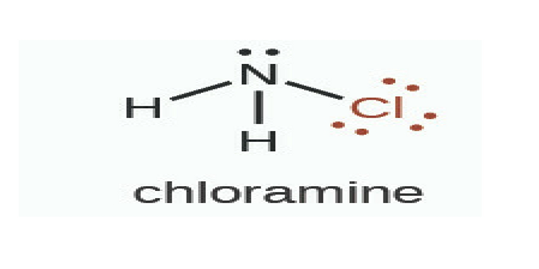
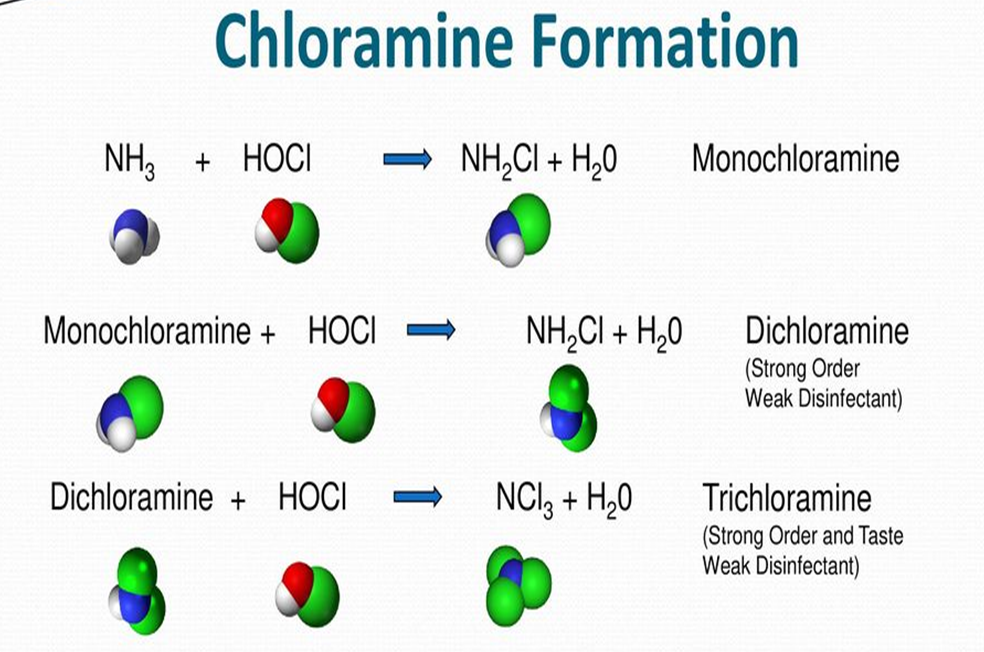
Chloramines are a group of chemical compounds that contain chlorine and ammonia.
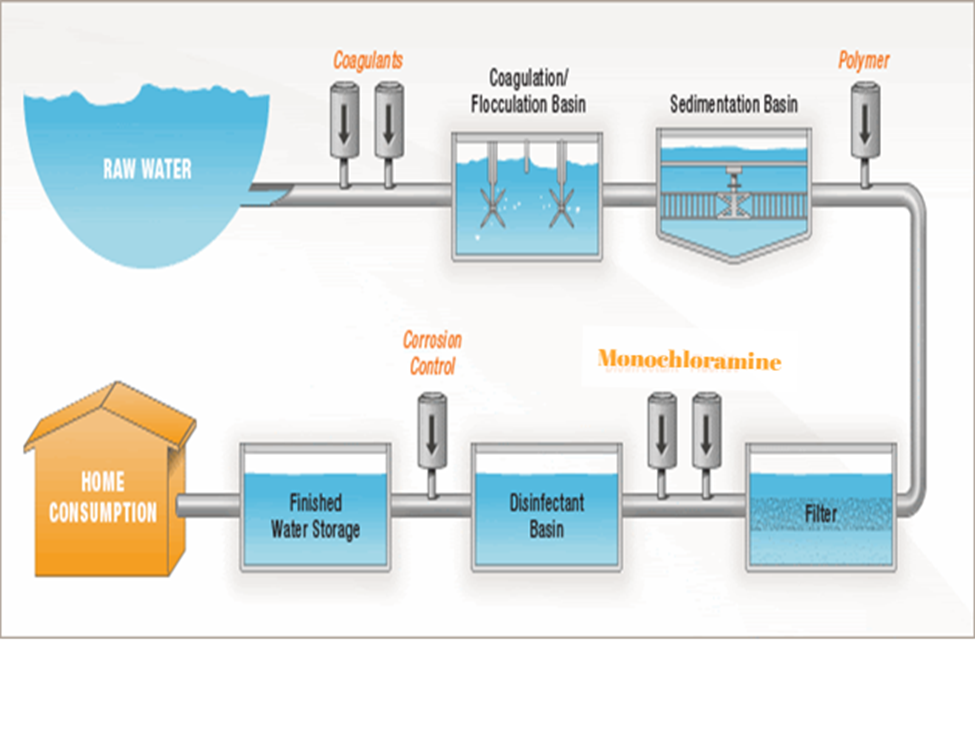
The particular type of chloramine used in drinking water disinfection is called monochloramine which is mixed into water at levels that kill germs but are still safe to drink.
pH and Monochloramine
Safe levels of Chloramine in water
CHLORINE VS MONOCHLORAMINE
| S.NO | CHLORINE | CHLORAMINE |
| 1 | Chlorine is a gaseous compound having a yellow green color and it is a toxic gas. | Chloramine is a gaseous compound and it is comparatively less toxic gas. |
| 2 | Chlorine dissipates and evaporates into the air quickly. Chlorine will usually evaporate after sitting for 24 hours. | Chloramine is more stable and will last longer in the water system. |
| 3 | Chlorine inactivated, no power to kill microbes at end of water delivery pipe. | Chloramine still present, killing microbes at end of water delivery pipe. |
APPLICATIONS
DRINKING WATER
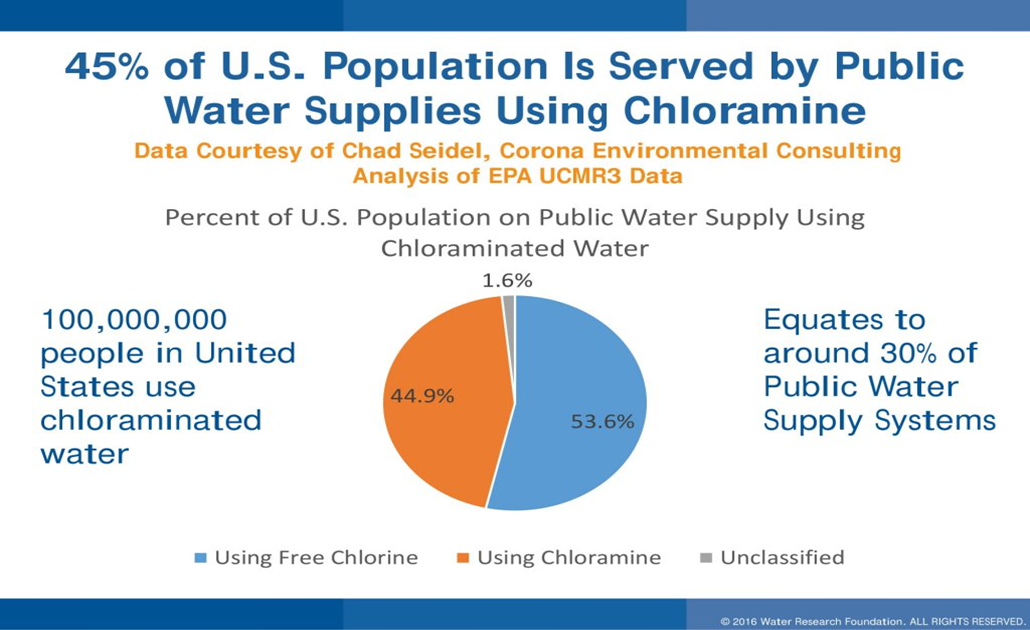
Chloramine has been used as a drinking water disinfectant in the United States in places like Cleveland, Ohio, Springfield, Illinois, and Lansing, Michigan since 1929. In 1998, an EPA survey estimated 68 million Americans were drinking water disinfected with chloramine. Several major U.S. cities such as Philadelphia, San Francisco, Tampa Bay, and Washington, D.C. use chloramine to disinfect drinking water. Chloramine is recognized as a safe disinfectant and a good alternative to chlorine.
More Information
EPA: Drinking Water Regulationsexternal icon
EPA: Drinking Water Treatability Databaseexternal icon
EPA. Chloramines in Drinking Waterexternal icon
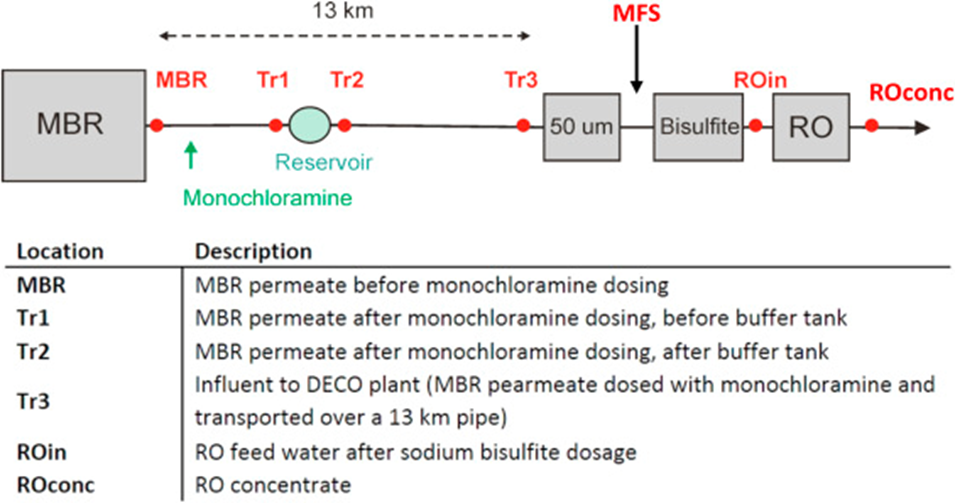
Monochloramine for wastewater reuse
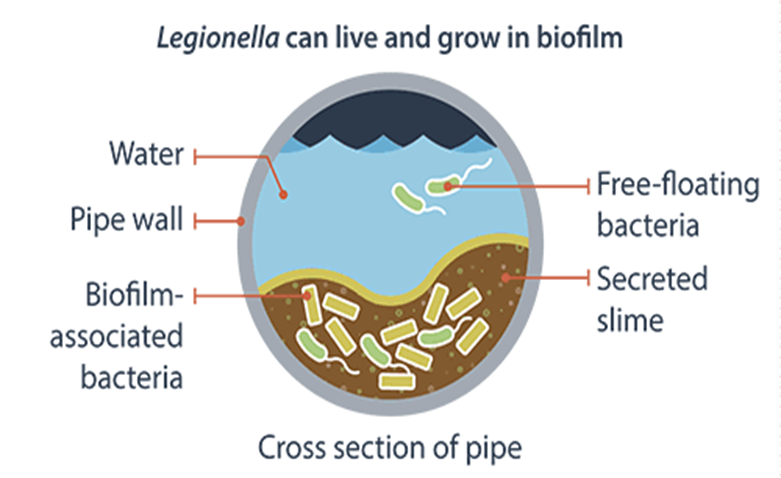
Legionella growth and spread
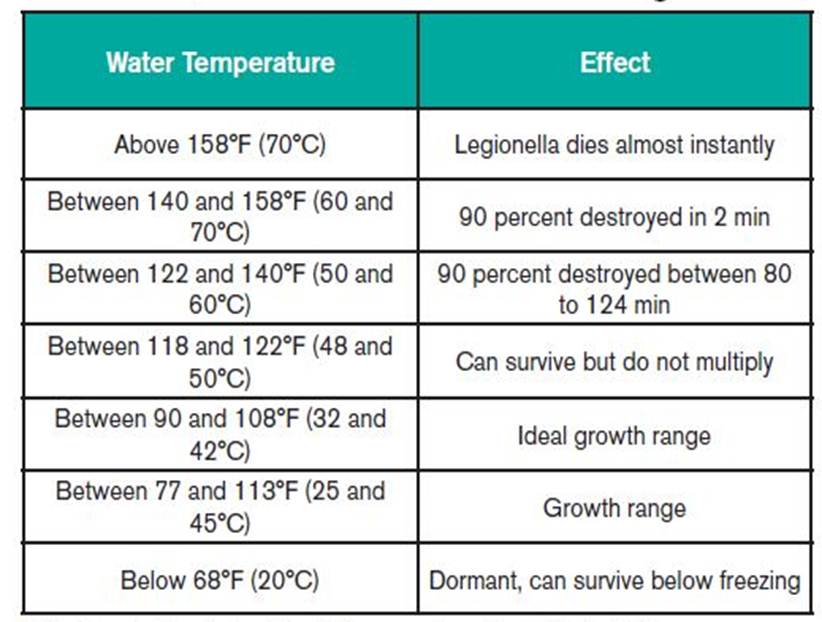
Temperature affects the survival of Legionella
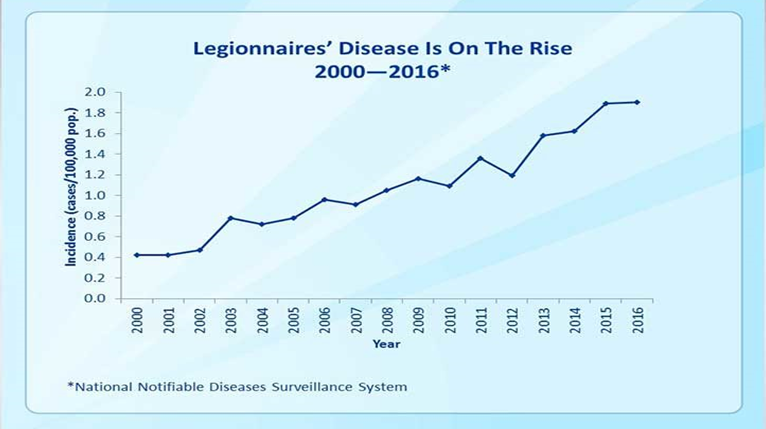
Monochloramine Use for Prevention of Legionella
EU
The European drinking water guideline does not contain standards for chloramines. When chloramines are used, few disinfection byproducts, such as trihalomethanes, are formed. However, other disinfection byproducts can form. Examples are toxic halonitrils (cyano chloride), halonitromethanes (chloropicrin) and other nitrogen-rich compounds. Some of these compounds can endanger human health. When the European Drinking Water Directive is revised, standards for these compounds will be added.
USA
According to American guidelines by EPA, drinking water that is treated with chloramines can contain a maximum amount of 4 mg/L Cl2. (National Primary Drinking Water Regulations EPA, 2002)
WHO
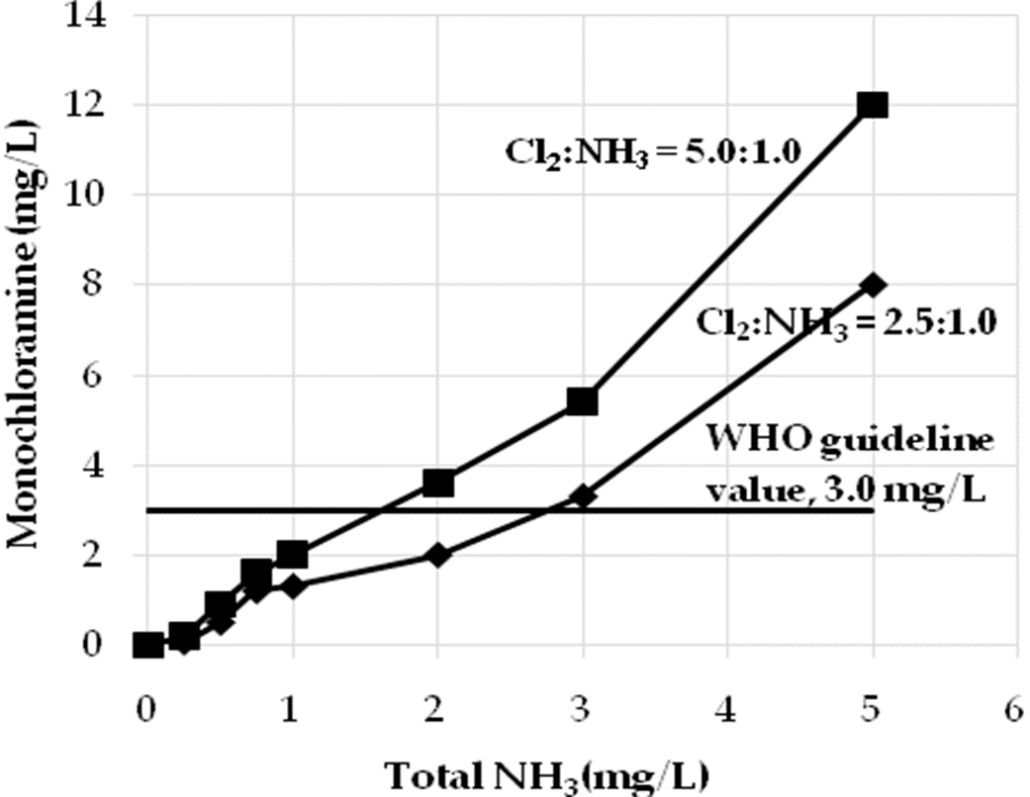
The WHO (World Health Organization) only dictates a standard for monochloramine as a disinfectant. The standard is 3 mg/L. For di- and trichloramine there are no standards, because the available information is not satisfactory for the establishment of a health guideline. (WHO, Guidelines for drinking-water quality – 3rd edition. Chemical aspects).

CHEMZEST introduces itself as a Manufacturer & supplier of Engineering Products & Specialty chemicals to various industries like Power Plants, Chemical/Pharma industries, Automobile industries & Plastic Industries.